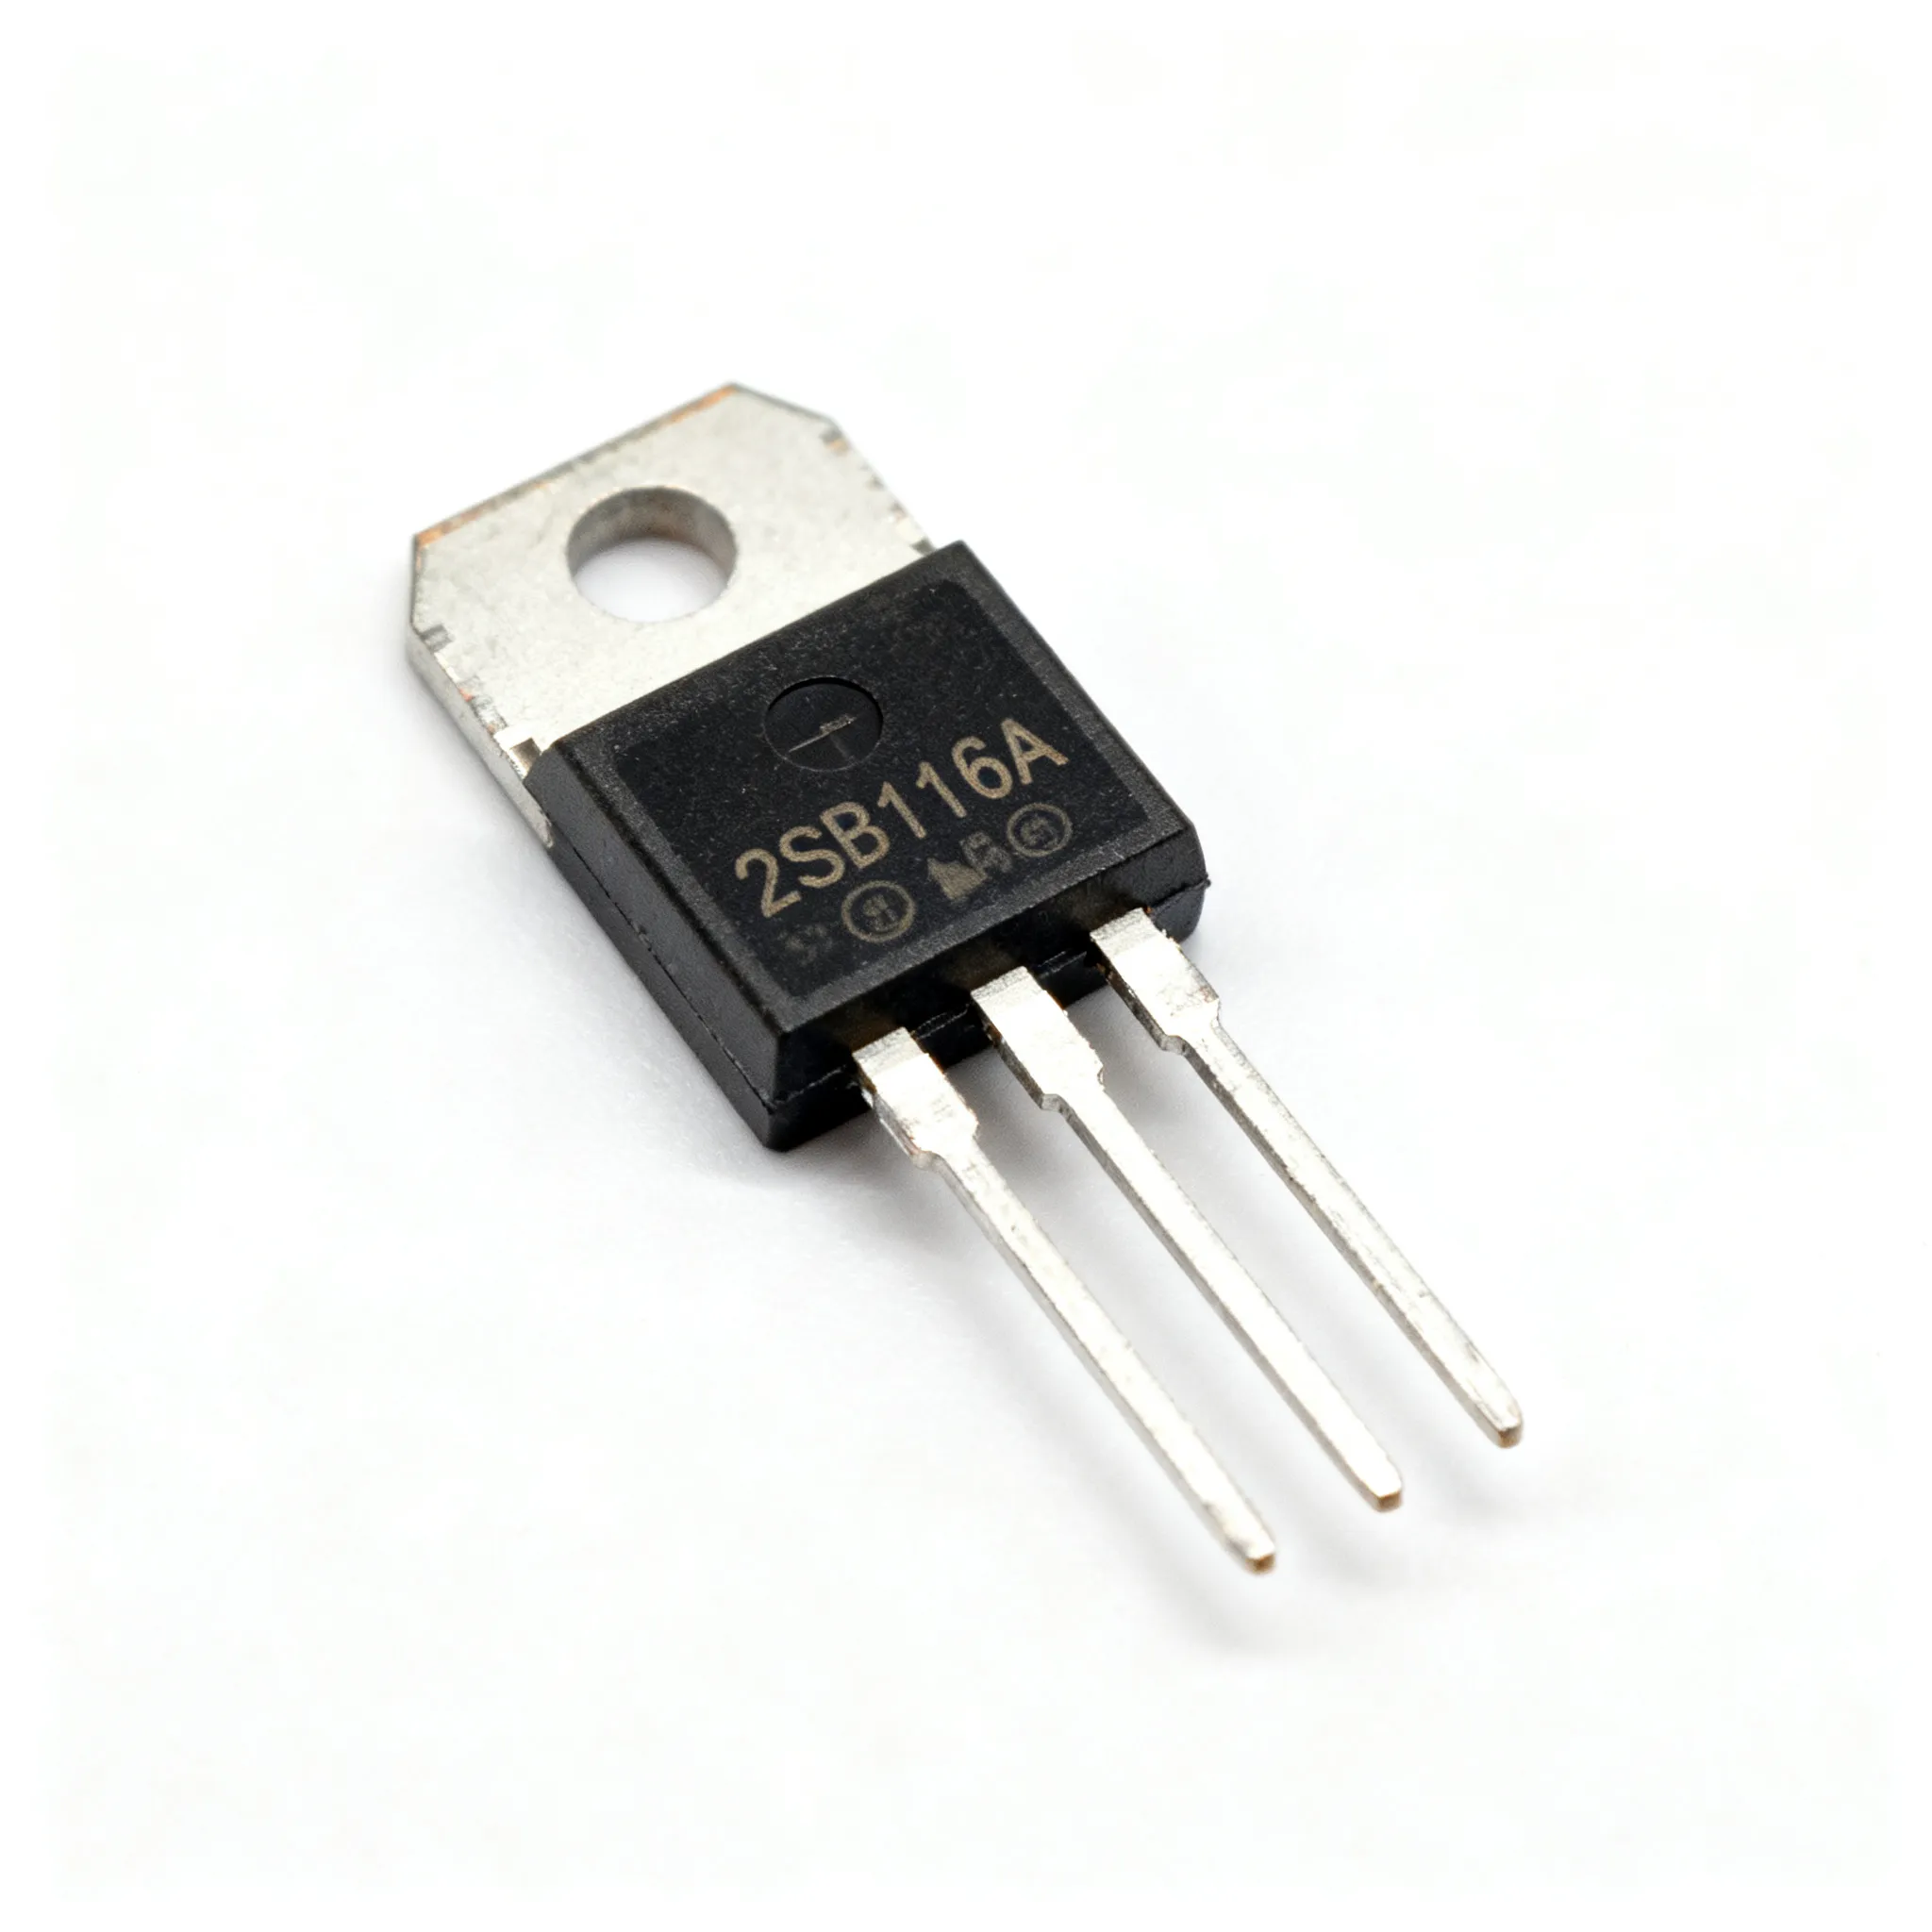
Obsolete Semiconductors: A Proactive Approach to End-of-Life Management for OEM Component Engineers
Practical guide for buyers and engineers: Obsolete Semiconductors: A Proactive Approach to End-of-Life Management for OEM Component Engineers. Sourcing, risk, and selection notes.
Why Waiting for a PCN Is No Longer Enough in the EOL Crisis
Component engineers and OEM buyers who have spent a decade managing bill‑of‑materials risk know the familiar rhythm: a product‑change notification arrives, then a scramble begins. In 2015, the average semiconductor lifecycle was still long enough to give procurement a comfortable lead time. Today, the pace of fab‑line consolidation, wafer‑process migration, and margin‑driven portfolio pruning has compressed that window to a handful of quarters — sometimes less. When you are supporting an industrial motor drive designed for a 15‑year field life, or a medical imaging system that must stay serviceable for a decade, a single EOL notice can blow a hole through your production plan.
The Dasenic obsolete components report documents a steep acceleration in end‑of‑life declarations — not just among niche ASICs, but across the analog, mixed‑signal, and discrete power semiconductors that form the backbone of long‑life equipment (IC Online, 2025). When those parts slip from “active” to “last‑time‑buy,” the aftermarket becomes the only channel; counterfeit risk escalates rapidly, and allocation‑backed lead times become a memory. As the IC‑Online sourcing guide on BOM health monitoring makes clear, “Proactive BOM health monitoring — using tools that ingest PCN data and correlate it with your AVL — is the only way to avoid being caught off guard.” (IC Online).
Yet many teams still treat a PCN like an alarm clock: they wake up only when it rings. By the time the distributor’s email lands, the manufacturer has already transferred capacity to a newer node, couponed wafers are exhausted, and the best allocation slots are gone. The reactive approach — checking inventory, rushing an RFQ, and hoping a grey‑market tray is genuine — is no longer a strategy; it’s a gamble. Proactive EOL management starts by assuming that every mature part is a future problem, and then building a system that catches the faint signals before they become emergencies.
Decoding Semiconductor Lifecycle Milestones Before They Disrupt Your Production
Component lifecycle management (CLM) is not a one‑time audit; it’s a continuous discipline that maps every part on the approved vendor list to a defined stage, then prescribes specific actions for engineering and procurement. Z2Data’s obsolescence management framework emphasizes that CLM involves “actively monitoring and managing the lifecycle of electronic components, from design and procurement to deployment and eventual end‑of‑life (EOL) phase.” Sourceability reinforces the point with its focus on digital transparency, noting that proactive obsolescence management can strengthen product design while digital solutions “ensure long‑term stability through greater transparency.” The table below translates those principles into concrete milestones.
| Lifecycle Stage | Typical Trigger / Indicator | Engineering Action | Procurement Action |
|---|---|---|---|
| Active | Full production volume; no manufacturer roadmap red flags | Capture complete datasheet, timing, and thermal profile; study fab‑process lineage | Maintain franchised source relationships; request allocation‑backed lead‑time confirmations via RFQ |
| Not Recommended for New Designs (NRND) | NRND flag in manufacturer portal; shrinking order books; fab node retirement hinted | Begin form‑fit‑function alternate selection; run simulation with candidate parts | Confirm NRND status with supplier; start bridge‑buy scenario analysis |
| EOL Announcement | Official PCN published; last‑time‑buy and last‑time‑ship dates set | Finalize substitute qualification; update BOM in PLM; evaluate firmware implications | Execute lifetime‑buy calculation; secure allocation‑backed order; require traceability documentation |
| Last‑Time‑Buy (LTB) | LTB window open; orders accepted but capacity limited | Freeze design; document any LTB‑stock storage and moisture‑sensitivity requirements | Place final orders with franchised distributors; require 90‑day test reports and full‑batch traceability |
| Obsolete | No further authorized production; market supply shrinks to residual stock | Maintain validated aftermarket sources; assess redesign trigger if failure rate increases | Source only through authorized aftermarket programs; third‑party lab testing mandatory for every lot |
The distinction between reacting to a PCN and practising CLM is dramatic. A PCN tells you the window is already closing; proactive monitoring — ingesting NRND flags, fab‑process change notices, and distributor allocation signals — gives you quarters, not weeks, to respond. When you build that data pipeline, the EOL crisis transforms from a fire drill into a managed engineering change.
Proactive Monitoring vs. Reactive Scrambling: Two Paths When a Part Goes End‑of‑Life
The military‑embedded community has been on the front line of obsolescence for decades, and their experience offers a stark warning for commercial OEMs. The article “Obsolete Semiconductors: A Proactive Approach to End‑of‑Life” notes that “the EOL schedule does not typically support the continuing needs of all of its customers, especially those serving applications with long system life cycles.” (Military Embedded Systems, 2024). When your elevator controller or railway signalling board depends on a 10‑year‑old discrete gate driver, the manufacturer’s EOL timeline is almost certainly shorter than your own.
The table below contrasts the proactive and reactive paths, highlighting where cost and schedule penalties accumulate.
| Decision Factor | Proactive EOL Management | Reactive (Post‑PCN) Scramble | Selection Note / Failure Boundary |
|---|---|---|---|
| Detection timing | Through automated BOM scanning that correlates PCN, NRND, and fab‑change feeds months before official EOL | When PCN lands, often 90–180 days before LTB closure | Early detection preserves 2‑3x the decision runway for qualification and negotiation |
| Alternate identification | Candidates evaluated and bench‑tested against original datasheet parameters (pinout, voltage thresholds, timing) while the original part is still available for side‑by‑side comparison | Rushed datasheet checks; samples often unavailable; “compatible” claims unverified until after LTB | Without side‑by‑side validation, subtle differences in ESD robustness or gain‑bandwidth can surface in the field |
| Procurement negotiation | Buyer uses competitive RFQ across franchised distributors and authorized aftermarket programs; can structure bridge‑buy or schedule orders to match production ramp‑down | Single‑supplier dependency; market allocation already consumed; forced to accept unknown open‑market stock | Proactive buyers confirm allocation‑backed lead time via RFQ; reactive buyers gamble on residual inventory |
| Counterfeit risk | Parts sourced through franchised/authorized channels with full traceability; lot‑specific test reports required | High reliance on unverified independent distributors; testing skipped under schedule pressure | IC‑Online guide: always require third‑party electrical compliance testing when outside franchised chain |
| Engineering burden | Structured redesign (if necessary) integrated into NPI roadmap; firmware adjustments planned | Emergency redesign forced into current sprint; regression testing rushed; potential field recall | The cost of a field‑replacement program dwarfs any “saving” from skipping proactive qualification |
| Total cost of ownership | Lower: bridge‑buy sized precisely; inventory carrying costs minimized; no line‑down events | Higher: premium pricing for last‑minute buys, line stoppages, requalification after counterfeit incident | Factor moisture‑sensitivity (MSL) re‑bake and storage cost over 10‑year life when calculating bridge‑buy |
The data‑driven path is not about spending more; it’s about spending earlier, when options still exist. Once a part moves to obsolete status, the open market escalates counterfeit risk dramatically, and lead times become entirely unpredictable. By contrast, a proactive posture keeps you in control of the qualification and sourcing timeline — exactly what an OEM component engineer needs when the BOM includes 300 lines and the next revision is two years away.
From GaN Drivers to Legacy Op Amps: How to Build an Obsolescence‑Resilient BOM
Building a BOM that can absorb EOL shocks without triggering a production stoppage is not a one‑time checklist; it’s an ongoing engineering practice. The following steps, refined from field experience with industrial and medical OEMs, convert the principles of proactive CLM into daily work instructions for component engineers and procurement buyers.
- Run a lifecycle audit on every approved vendor list line item. Export the AVL and assign each MPN a lifecycle score based on the manufacturer’s official status, age of the process node, and any NRND indicators listed in the distributor portal. Parts flagged as NRND or with a last‑production‑order date within 36 months should move to a watch list. Tools that correlate PCN/EOL data across multiple suppliers — such as BOM‑health platforms offered by independent distributors — can automate this scan weekly or monthly (Z2Data, 2024).
- Identify single‑source and high‑risk items. For every component where the AVL shows only one manufacturer and no franchised second source, verify single‑source risk through distributor documentation and manufacturer roadmaps. These line items are your top priority for alternate qualification. Even if you don’t qualify a second source today, begin evaluating candidate families — for example, GD32, APM32, or CH32‑class microcontrollers can be considered as potential substitutes for legacy STM32 parts, but verify pinout, package dimensions, and firmware compatibility under your actual edge conditions before listing them as alternates.
- Evaluate form‑fit‑function substitutes using original datasheets — not cross‑reference tables. The IC‑Online guide on defunct‑IC management makes this explicit: “When evaluating a substitute, always start with the original manufacturer datasheet, which outlines specifications, operating characteristics, and physical dimensions. Cross‑reference pinout, package, voltage tolerances, temperature range, and timing parameters before assuming compatibility.” Two parts that share a JEDEC package drawing can still differ in bond‑wire metallization, which affects electromigration life in a high‑current gate‑driver application. Use the table below as your verification checklist.
- Qualify the alternate source while the original part is still available. Order samples of the candidate part and test it side‑by‑side with the OEM device under your system’s worst‑case conditions: maximum ambient temperature, lowest input voltage, full inrush current, and worst‑case EMI profile. Only after passing those tests should the alternate be assigned a temporary internal part number and added to the AVL as a contingent source. This parallel‑qualification window is the single largest cost‑saver in the entire EOL workflow.
- Structure the bridge‑buy and storage plan. Once you have a qualified alternate, the lifetime‑buy decision becomes a financial equation, not an emotional one. Calculate the total cost of the bridge‑buy (part cost plus MSL‑bake, dry‑storage, and periodic retesting) versus the re‑engineering cost of accelerating the alternate’s qualification. For low‑volume, safety‑critical functions where a redesign could trigger a 12‑month agency re‑certification, a bridge‑buy often wins. For high‑volume lines, moving to the alternate early may be cheaper than storing thousands of MSL‑3 devices.
| Substitution Verification Parameter | What to Compare | Why It Matters | Reference Document |
|---|---|---|---|
| Package outline & footprint | Millimeter dimensions, pin‑1 location, exposed pad size | A 0.2 mm pad shift can create solder‑bridging or thermal‑pad voiding | Original OEM datasheet, JEDEC package drawing |
| Pinout & pin function | Every pin: power, ground, I/O, NC, RSVD | Internal pull‑up/down differences, missing RESET pins, or redefined NC pins that are actually test‑mode entry | OEM datasheet vs. candidate datasheet |
| Supply voltage range & tolerance | VDD min/max, ramp‑rate requirements | A part rated for 3.3 V ±5% may brown‑out at 3.0 V in your system if you use a 3.0‑3.6 V range; the original might tolerate 2.7 V | OEM datasheet electrical characteristics table |
| Timing parameters | Propagation delay, setup/hold, rise/fall time, clock tolerance | An op‑amp with 1.5× the specified slew rate may oscillate in an integrator circuit; a slower digital isolator may violate I²C bus timing | Switching characteristics section of OEM datasheet |
| Temperature range | Operating (Tamb), junction (Tj), storage | An industrial part rated for –40 to +85 °C cannot replace a –40 to +125 °C automotive‑grade device in an outdoor enclosure | OEM datasheet absolute maximum / recommended operating conditions |
| Thermal resistance (θJA, θJC) | JEDEC standard values under defined PCB layout | Even identical‑looking SO‑8 packages can differ by 20 °C/W if one uses a fused‑lead technology | OEM datasheet thermal characteristics |
| EMI & noise profile | Output ringing, conducted emissions, PSRR over frequency | A switching regulator substitute may meet efficiency specs but inject 10 dB more noise into the analog rail | Bench‑measurement, not datasheet alone |
Every column in that table represents a failure that we have seen in the field — a microcontroller that latched up because the “NC” pin was actually a test mode, a GaN driver that failed after 300 hours because its bond‑wire diameter was thinner, a legacy op‑amp whose substitute introduced 5 mV of offset that pushed analog calibration out of spec. Proactive verification is tedious, but it’s the only way to avoid turning a pin‑compatible label into a field‑returns statistic.
Straight Answers to the Hard Questions About Obsolete Semiconductor Management
After years of managing component EOL strategies across industrial, medical, and transportation OEMs, I’ve found that the same five questions surface in every engineering‑procurement meeting. Here are the answers that actually change behaviour.
- Q: How frequently should I run a lifecycle scan on my BOM if I’m supporting a 15‑year industrial product?
Quarterly scans are the absolute minimum. High‑risk systems — those with a large share of mature analog, discrete power, or mixed‑signal parts whose fabs are known to be transitioning to 300 mm or retiring legacy process nodes — should move to monthly automated scans. The scan must ingest PCN and EOL feeds and correlate them with your AVL so that parts entering NRND status or showing fab‑process changes are flagged before the official notice reaches procurement. By the time the PCN lands, the manufacturer has typically already aligned its wafer allocation; a quarterly scan that misses that precursor simply hands your competition the available LTB slots. - Q: Can I rely solely on manufacturer PCN alerts to stay ahead of obsolescence?
No. PCNs have short timeframes — sometimes as little as 90 days between notification and last‑time‑buy closure — and they often arrive after internal engineering teams have already de‑risked their own NPI pipeline. To catch the subtle signals, you need proactive CLM tools that aggregate data across multiple suppliers and map it against your AVL. Fab‑process change notices, NRND flags on distributor portals, and softening order books all precede formal EOL; a PCN‑only approach misses every one of them. Sourceability’s digital‑solutions perspective reinforces that transparency across the supply chain is the key to early detection — waiting for a single manufacturer email is the opposite of transparency. - Q: What is the safest way to buy obsolete semiconductors without getting counterfeits?
Work exclusively through franchised distributors that offer authorized aftermarket programs, or through independent distributors who can supply full traceability documentation and third‑party laboratory testing for each lot. When a part is truly obsolete and no franchised stock remains, require the following from any independent source: a Certificate of Conformance that ties each reel or tray to a specific OEM wafer‑lot number, a test report generated within the last 90 days by an ISO‑17025‑accredited lab verifying electrical compliance to the original manufacturer specifications, and a written guarantee of authenticity with a no‑questions‑asked replacement policy. Never buy from unverified open‑market sources unless you are prepared to perform X‑ray inspection, decapsulation, and electrical curve‑trace analysis on every lot. The counterfeit risk escalates exponentially once a part disappears from authorized channels (IC Online, 2025). - Q: When does it make sense to redesign a board around a new ASIC instead of stockpiling an obsolete part?
Calculate the total cost of a lifetime buy — including purchase price, MSL‑sensitive storage (dry cabinets, re‑bake cycles), inventory carrying cost over the remaining production life, and the potential need for re‑qualification if the stored parts show solderability degradation. Compare that against the re‑engineering cost of designing in a newer pin‑compatible or functionally equivalent part, factoring in PCB re‑spin, firmware changes, and regulatory re‑certification. If annual usage is low (hundreds of units per year) and the original part’s packaging technology is becoming unavailable at any foundry — for example, a ceramic DIP driver that no fab will manufacture — a redesign is almost always cheaper than storing COTS parts for a decade. For safety‑critical functions, the decision tilts further toward redesign because long‑term storage introduces uncontrolled variables that can erode reliability margins. - Q: How do I evaluate a drop‑in substitute when the original semiconductor’s datasheet doesn’t tell the whole story?
Start with the OEM datasheet for pinout, voltage thresholds, timing, and thermal curves — that’s your baseline. Then test the candidate under your system’s actual edge conditions: full inrush current at minimum input voltage, maximum ambient temperature with worst‑case airflow, radiated and conducted EMI profile, and representative dynamic loading. Even parts with identical top‑mark part numbers may come from different wafer fabs or use different metallisation stacks; a shift from aluminium to copper bond pads, for instance, can change wire‑bond reliability in high‑vibration environments. When evaluating analog or mixed‑signal parts, pay special attention to parameters that are not guaranteed by datasheet limits but are critical to your circuit, such as phase reversal behaviour during overdrive or start‑up overshoot. The IC‑Online guide on EOL ICs keeps emphasising: the datasheet is a starting point, not a substitute for at‑temperature electrical characterisation on your own board.
References & Further Reading
- Sourcing End‑of‑Life and Obsolete Semiconductors: A Practical Guide for OEM Buyers and Component Engineers – IC Online
- End‑of‑Life Integrated Circuits: What OEM Buyers and Component Engineers Need to Know – IC Online
- Obsolete Semiconductors: A Proactive Approach to End‑of‑Life – Military Embedded Systems
- Semiconductor Obsolescence Management Best Practices – Z2Data
- How to Mitigate Electronic Component Obsolescence Risks – Sourceability
Conclusion
Managing obsolete semiconductors is not a procurement problem — it is a system‑engineering discipline that starts long before a PCN arrives. By moving lifecycle scans from an annual audit to a continuous, automated function, qualifying alternates while the original part is still on the shelf, and treating every NRND flag as a warning rather than an afterthought, OEM component engineers can decouple production schedules from the unpredictable decisions of a handful of wafer fabs. The tools exist, the data feeds are available, and the cost of not using them is measured in line stoppages, fraudulent parts, and redesigns that could have been avoided. The only question left is whether your team will act before the next EOL notice — or after.
Take the next step. Upload your full BOM on IC‑Online to trigger a proactive lifecycle audit and request a consolidated quote. IC‑Online handles mixed BOMs with flexible MOQs, and the RFQ includes allocation‑backed lead‑time confirmation and traceability documentation — so you spend less time chasing obsolete parts and more time engineering resilient systems.